As manufacturing and logistics industries continue to automate production processes, the demand for efficient and reliable material handling equipment is rapidly increasing. A conveyor belt system plays a critical role in improving workflow efficiency, reducing manual labor, and optimizing production operations.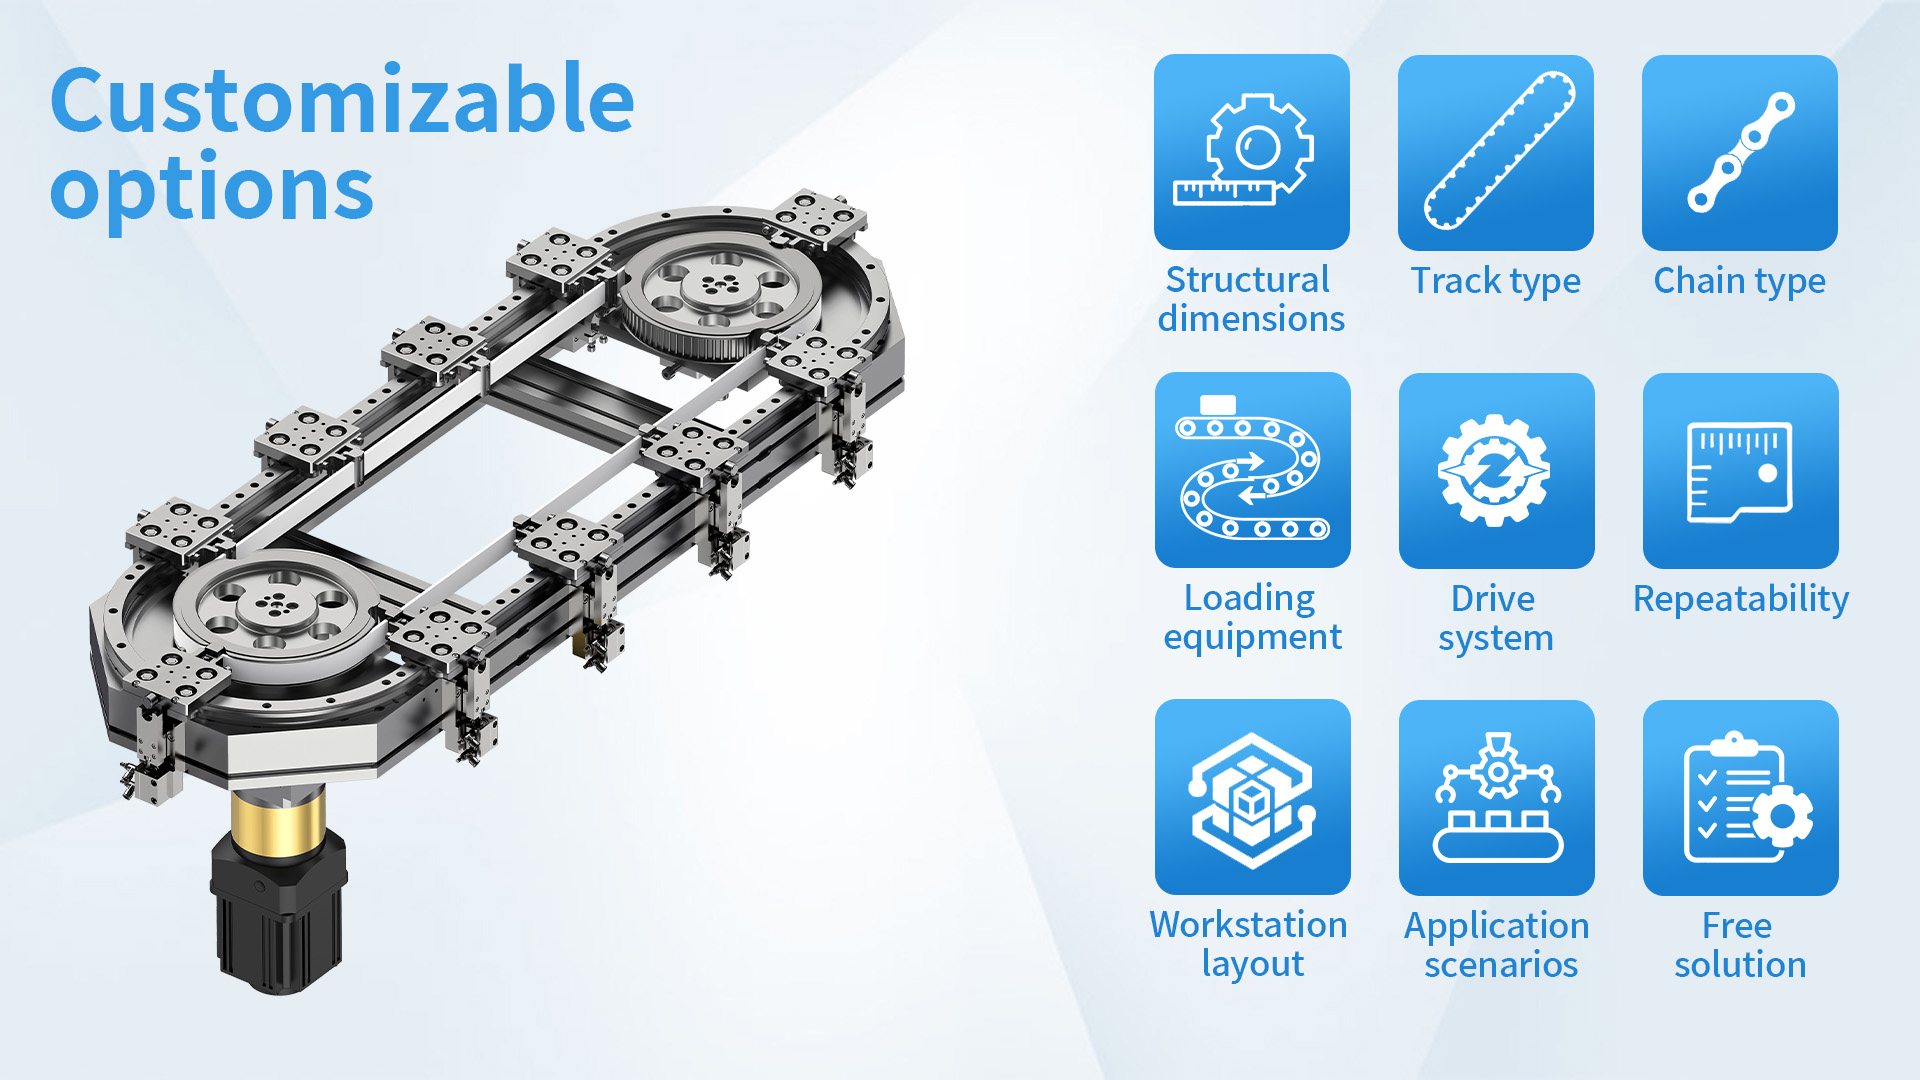
For OEM manufacturers, factory automation companies, and system integrators, customized conveyor belt system solutions provide the flexibility and performance required for modern industrial applications.
A conveyor belt system is a mechanical handling system designed to transport products, materials, or components efficiently from one location to another. It is widely used in manufacturing, packaging, warehousing, and automated production environments.
Typical system components include:
Conveyor systems can be designed for continuous transport, indexing movement, or synchronized automation processes.
Standard conveyor systems may not always meet the specific layout, speed, or production requirements of industrial automation projects. This is why many companies choose custom conveyor belt system solutions.
Customization options include:
Custom systems improve production efficiency while maximizing factory space utilization.
Automates material transportation and reduces manual handling.
Can be customized for different industries and production layouts.
Industrial-grade designs support continuous operation.
Compatible with robots, PLC controls, vision systems, and smart factory platforms.
Automation minimizes manual intervention and improves workflow consistency.
Industrial conveyor belt systems are widely used across multiple industries:
Supports automated product movement between workstations.
Improves efficiency in packaging and logistics operations.
Provides hygienic and efficient material transport.
Supports precision handling of sensitive components.
Automates material flow and inventory handling.
Different industries require different conveyor configurations.
Ideal for continuous material transport and general production lines.
Provides accurate stop-and-go positioning for assembly automation.
Flexible structure for easy expansion and maintenance.
Designed for large loads and industrial environments.
Modern automated conveyor systems can be integrated with:
This enables intelligent and synchronized manufacturing processes.
When selecting a supplier for conveyor belt system solutions, consider:
A professional supplier can help optimize workflow efficiency and long-term operational performance.
As industries continue to adopt smart manufacturing technologies, efficient material handling systems are becoming more important than ever. A conveyor belt system provides the reliability, flexibility, and automation capability required for modern industrial operations.
By partnering with an experienced manufacturer, OEM companies and automation integrators can develop custom conveyor solutions tailored to their production requirements and future automation goals.